Quick Answer
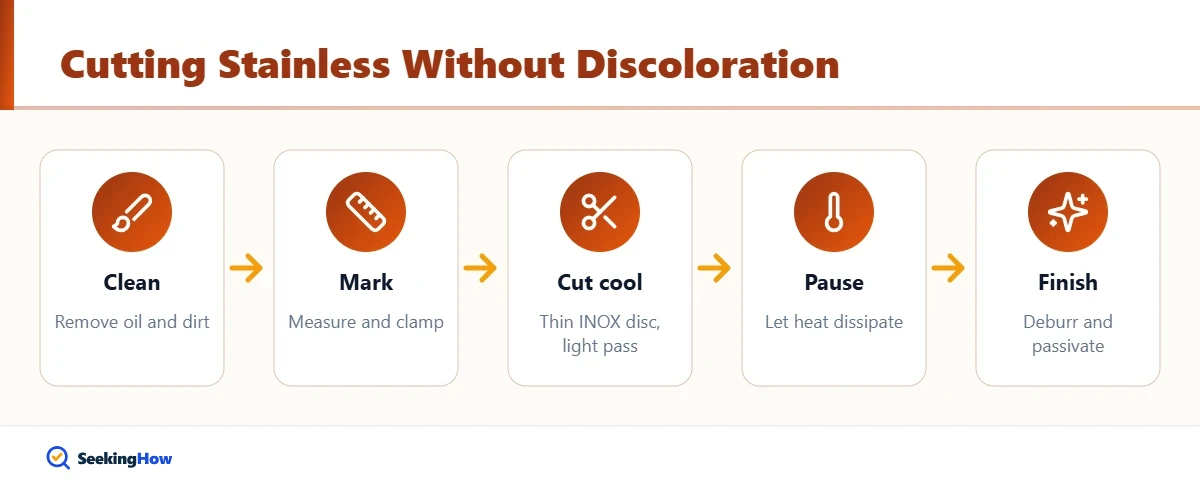
To cut stainless steel without discoloration, keep heat out of the cut: use a thin 1 mm INOX-rated cut-off disc or a carbide metal-cutting blade at the right speed, apply light pressure, cut in short passes, cool with cutting fluid, and use clean, stainless-only tools. For sheet metal, cold methods like aviation snips, nibblers or shears avoid heat tint entirely.
Key Takeaways
- The blue, gold or brown colors on cut stainless are heat tint, an oxide layer caused by overheating.
- Thin INOX discs and low-RPM carbide or cold saws generate far less heat than thick abrasive wheels.
- Cold-cutting tools such as snips, nibblers and shears leave no heat tint at all on thin sheet.
- Tools that touched carbon steel can embed iron particles that later rust, so keep stainless-only discs and brushes.
- Light heat tint can be removed with a stainless cleaner or non-woven pad; heavy tint needs pickling or electrochemical cleaning.
Stainless steel stays stainless because of a thin, invisible chromium oxide layer on its surface. Too much heat during cutting thickens that oxide into visible colors and can reduce corrosion resistance right at the edge. Choosing the right tool and technique keeps your cuts bright, clean and rust-free.
Why Does Stainless Steel Discolor When You Cut It?
When stainless steel gets hot, oxygen reacts with the surface and builds a thicker oxide layer. Light thin layers look straw or gold; thicker layers look purple, blue and eventually dull gray or brown. This is called heat tint, and the hotter the metal gets, the darker the color.
Heat tint is more than cosmetic. The zone under the colored oxide can be lower in chromium, which weakens the passive layer that protects stainless from rust. On food equipment, marine hardware and outdoor railings, that is often where corrosion starts. A second cause of discoloration is contamination: abrasive discs or wire brushes previously used on mild steel leave iron particles that rust into orange specks within days.
Which Cutting Method Causes the Least Discoloration?
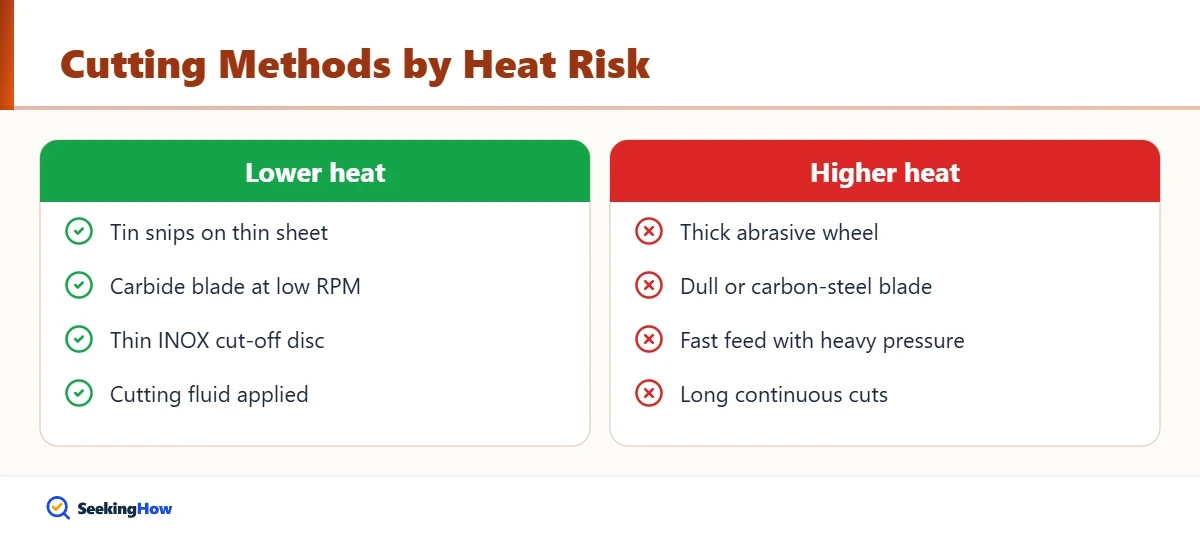
The best method depends on the thickness and shape of the material. The general rule is simple: the less friction heat a method produces, the less discoloration you get.
| Method | Heat Tint Risk | Best For | Notes |
|---|---|---|---|
| Aviation snips / hand shears | None | Thin sheet up to about 24-26 gauge stainless | Cold cut; use stainless-rated snips |
| Electric nibbler or power shear | None to very low | Sheet and curves | Leaves a small kerf or a clean sheared edge |
| Cold saw / carbide metal-cutting saw | Low | Tube, bar, angle, sheet | Low RPM; chips carry heat away |
| Bandsaw with bi-metal blade | Low | Tube, solid bar | Slow speed plus coolant |
| Angle grinder, 1 mm INOX disc | Moderate | Quick field cuts | Short passes, light pressure |
| Plasma cutter | High | Thick plate | Expect a heat-affected edge to clean up |
| Waterjet | None | Precision parts | Usually outsourced to a fabricator |
| Fiber laser with nitrogen assist | Very low | Production parts | Oxygen assist darkens edges; nitrogen keeps them bright |
What Tools and Supplies Do You Need?
- Thin cut-off discs labeled INOX (1 mm or 0.040 inch), which are formulated to be free of iron, sulfur and chlorine contamination
- Carbide-tipped metal-cutting blade rated for stainless, for a metal-cutting circular saw or cold saw
- Bi-metal bandsaw or reciprocating saw blades with a fine tooth count (14-24 TPI for thin wall)
- Cutting fluid or wax stick made for stainless
- Masking tape and a fine marker for layout
- Clamps and a sturdy work surface
- Stainless-steel wire brush and non-woven abrasive pads kept only for stainless
- Safety gear: safety glasses plus face shield, hearing protection, cut-resistant gloves and long sleeves
How To Cut Stainless Steel Without Discoloration
These steps apply to the most common home and small-shop tools: an angle grinder, a metal-cutting saw or a bandsaw.
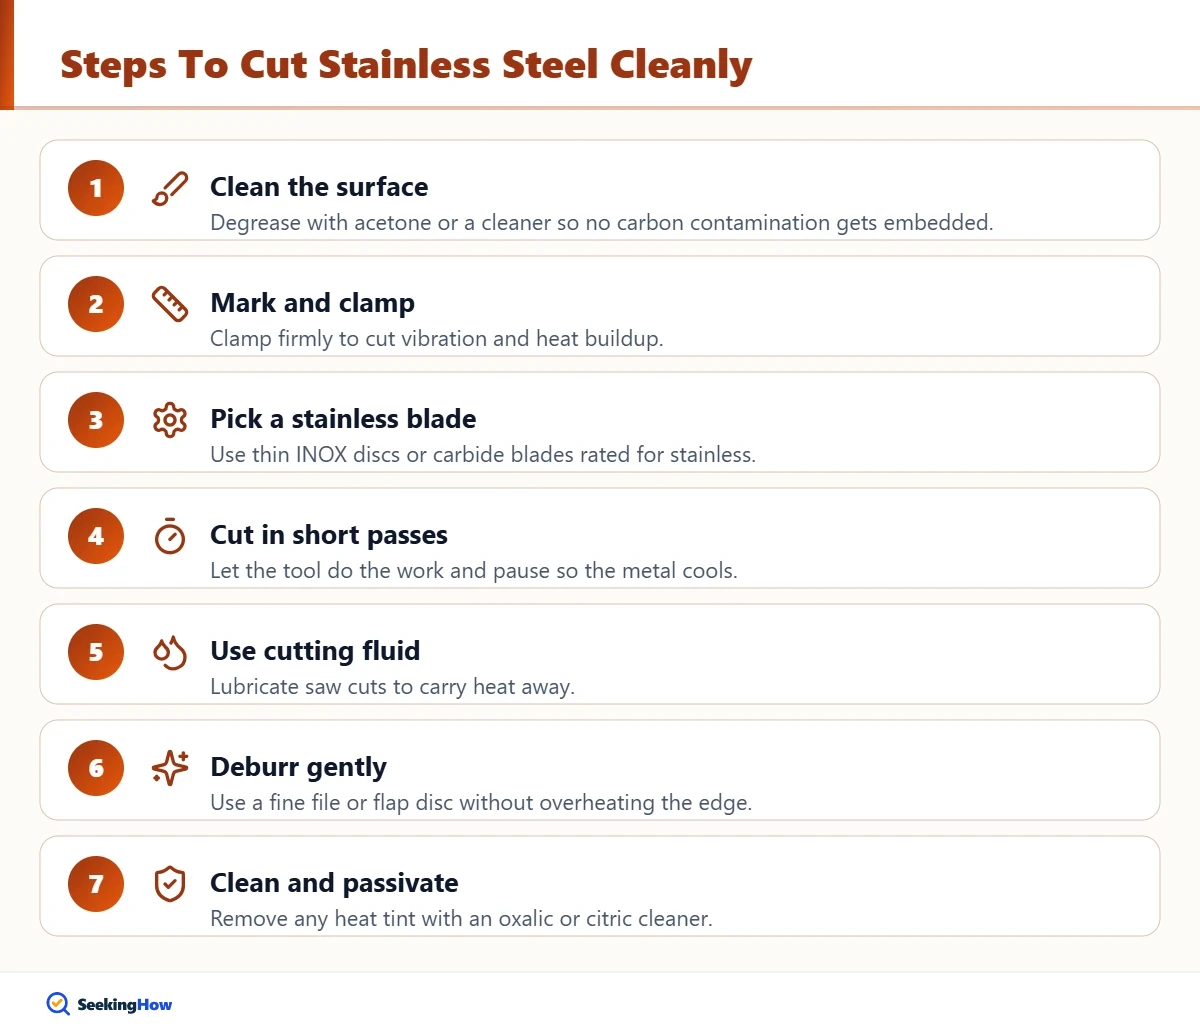
Step 1: Choose a Low-Heat Cutting Method
Match the tool to the job using the table above. For thin sheet, reach for snips or a nibbler first. For tube and bar, a cold saw, carbide metal-cutting saw or bandsaw beats a grinder for heat control.
Step 2: Use Clean, Stainless-Only Consumables
Install a new INOX disc or a stainless-rated blade that has never touched carbon steel. Label these tools and store them separately so they stay uncontaminated. Wipe the workpiece with a clean cloth and solvent to remove oil and shop grit.
Step 3: Mark and Protect the Cut Line
Lay masking tape along the cut and mark it with a fine marker. The tape protects the finish from scratches and spatter. Leave the protective plastic film on sheet stock until all cutting and drilling is finished.
Step 4: Clamp the Workpiece Firmly
Secure the stainless with clamps so it cannot vibrate. Vibration causes chatter, rubbing and extra friction heat, and it can also bind the disc or blade. Support long pieces on both sides of the cut.
Step 5: Apply Cutting Fluid
On saws and bandsaws, apply cutting fluid or a wax stick to the blade and cut line. Lubrication reduces friction and carries heat away. With an abrasive disc, skip liquid coolant on the disc itself and instead control heat with technique.
Step 6: Cut With Light Pressure and Short Passes
Let the tool reach full speed, then feed gently and let the disc or teeth do the work. Forcing the cut creates heat and glazes the disc. On thicker stock, cut a few seconds at a time and pause so the metal can cool; if the area is too hot to touch, wait longer.
Step 7: Deburr and Clean the Edge
Remove burrs with a file or a fine flap disc used only on stainless, working gently to avoid new heat. Wipe off cutting fluid and metal dust with a clean cloth. Inspect the edge for any color or embedded particles.
Step 8: Remove Any Heat Tint and Passivate
Treat light straw-colored tint with a stainless cleaner or a non-woven abrasive pad, rubbing in the direction of the grain. For heavier tint, use a pickling paste or an electrochemical weld-cleaning machine. Finish with a citric or nitric acid passivation product to rebuild the protective layer.
How Do You Remove Discoloration After Cutting?
Pick the gentlest method that works, because aggressive grinding can create new scratches and heat.
- Light tint (straw to gold): A paste cleaner with oxalic acid, such as a stainless-safe powdered cleanser, or a fine non-woven pad usually removes it.
- Moderate tint (purple to blue): Electrochemical weld-cleaning units use a mild electrolyte and current to remove oxide and passivate in one pass.
- Heavy tint (dark blue to gray): Pickling paste containing nitric and hydrofluoric acid is the industrial standard, but it is highly hazardous and best left to fabricators.
Safety: Pickling pastes containing hydrofluoric acid can cause severe chemical burns and systemic poisoning even from small skin exposures. Follow the safety data sheet exactly, or have a professional fabrication shop do the cleaning.
If orange specks appear days later, iron contamination is the usual culprit. The cleanup approach is similar to other surface rust; our guide to the fastest way to remove rust from metal explains gentle options, and for polishing other decorative metals see how to clean nickel silver.
Common Mistakes That Cause Discoloration
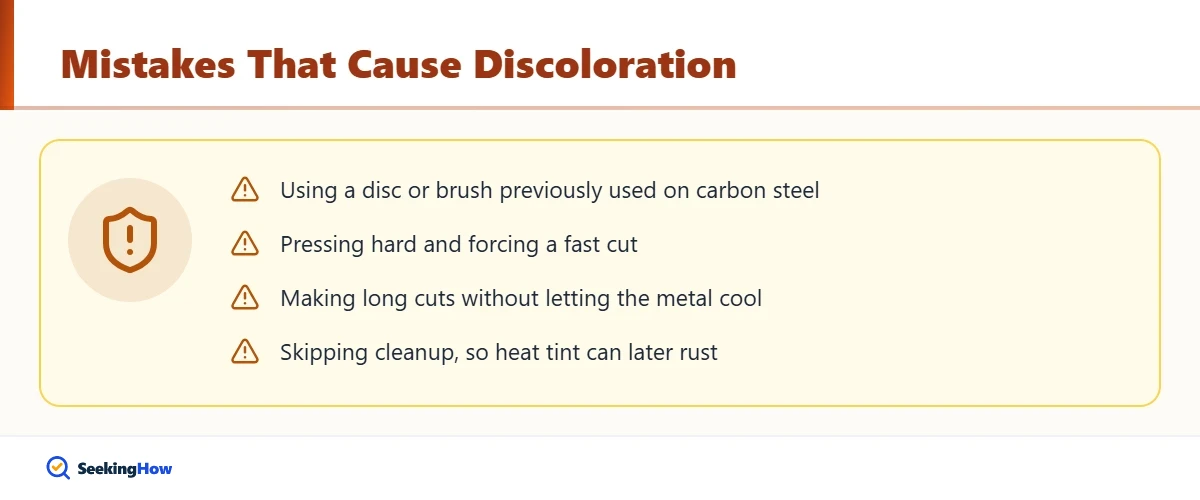
- Using a thick grinding wheel to cut. Wide wheels rub more metal and build heat quickly.
- Running a saw too fast. High blade speed on stainless causes work hardening and heat; follow the blade maker’s speed range.
- Pressing hard to finish faster. Pressure equals friction, and friction equals heat tint.
- Sharing discs and brushes with mild steel. Iron transfer causes rust spots that look like discoloration.
- Quenching hot stainless in water. It does not undo heat tint and can warp thin parts.
When Should You Have Stainless Steel Cut Professionally?
If you need perfectly bright edges on visible parts, such as backsplashes, appliance panels or architectural trim, a fabricator with a fiber laser, waterjet or shear can cut to size with little or no cleanup. The same goes for thick plate over about 1/4 inch, which is slow and hot to cut with handheld tools. Ordering cut-to-size stock is often cheaper than ruining expensive material.
Working with other hard-to-cut sheet materials? Many of the same principles, like sharp blades, firm clamping and gentle feed, apply when you cut corrugated plastic sheeting.
Frequently Asked Questions
What causes the blue color on cut stainless steel?
The blue color is heat tint, a thickened oxide layer that forms when stainless steel overheats during cutting, grinding or welding. Light heat makes straw or gold tones, while more heat produces purple, blue and gray. It can also lower corrosion resistance at the edge.
Can you cut stainless steel with an angle grinder?
Yes. Use a thin 1 mm cut-off disc labeled INOX, let the grinder reach full speed, and cut with light pressure in short passes. Clamp the workpiece and pause to let it cool. Expect a little heat tint that cleans up with a pad or stainless cleaner.
Does heat tint on stainless steel cause rust?
It can. The area under heavy heat tint may have reduced chromium at the surface, which weakens the passive layer. Removing the tint and passivating the edge restores protection, which matters most for outdoor, marine and food-contact parts.
What blade is best for cutting stainless steel?
For tube, bar and sheet, a carbide-tipped blade designed for stainless or a cold saw blade at low speed works well. Bandsaws need a bi-metal blade with a fine tooth pitch. For quick cuts with a grinder, use a thin INOX abrasive disc.
How do you remove heat discoloration from stainless steel?
Light discoloration usually comes off with an oxalic acid stainless cleaner or a fine non-woven pad rubbed along the grain. Darker tint needs an electrochemical weld cleaner or pickling paste. Finish by passivating with a citric or nitric acid product.